Battery-News

Author name: Redaktion

Battery Recycling in Europe

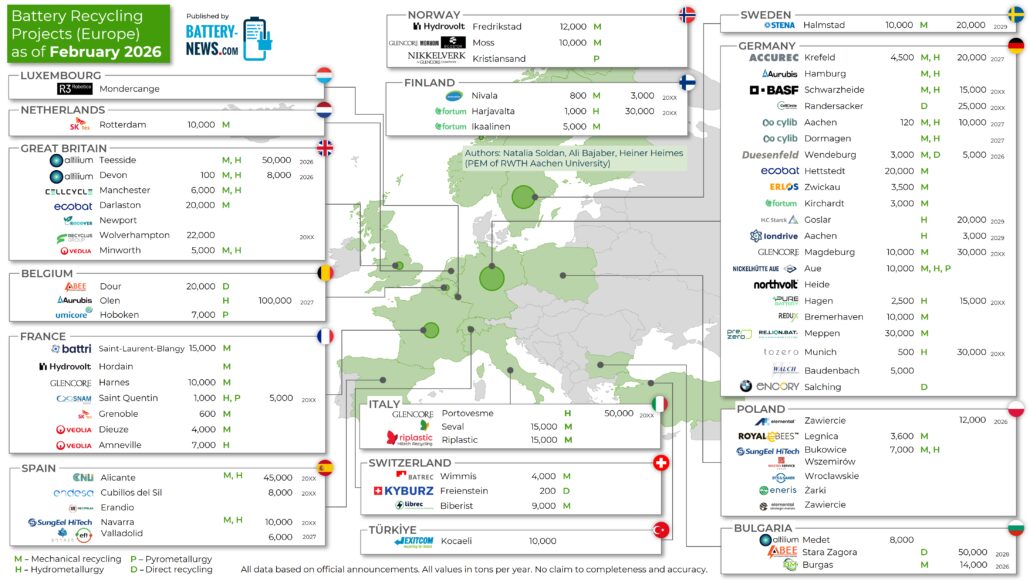
Battery-News presents an updated map of lithium-ion battery recycling in Europe in cooperation with the Chair of Production Engineering of E-Mobility Components (PEM) at RWTH Aachen University. The overview reflects the status as of February 2026 and was compiled by Natalia Soldan, Ali Bajaber, and Professor Heiner Heimes. Recycling Projects Across 15 European Countries The map shows planned and existing recycling projects, including their capacities and intended processes where specified. It distinguishes between mechanical, hydrometallurgical, pyrometallurgical, and direct recycling, illustrating both the geographic distribution and the different technological approaches within Europe’s recycling infrastructure. The overview covers projects across 15 European countries. Germany has the largest number of listed locations, with additional recycling activities in countries including the United Kingdom, France, Spain, Poland, and the Nordic countries. The map is available for free download in high resolution. This overview does not claim to be exhaustive. The editorial team welcomes corrections and additions through the contact form.

Battery Recycling in Europe Read More »

AMG Lithium opens solid electrolyte testing lab in Frankfurt

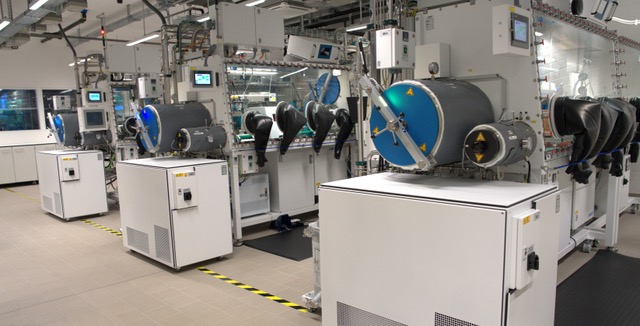
AMG Lithium has commissioned its “PerLa” performance lab in Frankfurt, Germany, to develop and test sulfide solid electrolytes for solid-state batteries. Equipped with more than 200 test channels for standard testing and detailed electrochemical analysis, the facility is intended to expand joint development work with customers and partners. A new glovebox line covers the entire production process for laboratory-scale battery cells, from electrode slurry preparation and coating to cell assembly and pouch packaging. All steps take place in a controlled inert atmosphere. The setup allows materials to be evaluated in battery cells representative of practical applications using standardized test protocols. The expansion added 250 square meters, bringing the total laboratory area to approximately 1,100 square meters. According to AMG Lithium CEO Stefan Scherer, the performance lab will support the market introduction of the company’s solid electrolyte technology and facilitate targeted collaboration with customers. Part of AMG Critical Materials, AMG Lithium develops battery-grade lithium hydroxide as well as materials for solid-state batteries. Sources:https://www.automobil-industrie.vogel.de/amg-lithium-eroeffnet-testlabor-festelektrolyte-frankfurt-a-dad21642e7a60832712b2425926f8d2f/https://www.next-mobility.de/amg-lithium-nimmt-testlabor-fuer-festelektrolyte-in-frankfurt-in-betrieb-a-c6325a78afa35a2f16caf30e24d84210/

AMG Lithium opens solid electrolyte testing lab in Frankfurt Read More »

Skellium Develops Lithium Metal Anodes Using Melt Coating

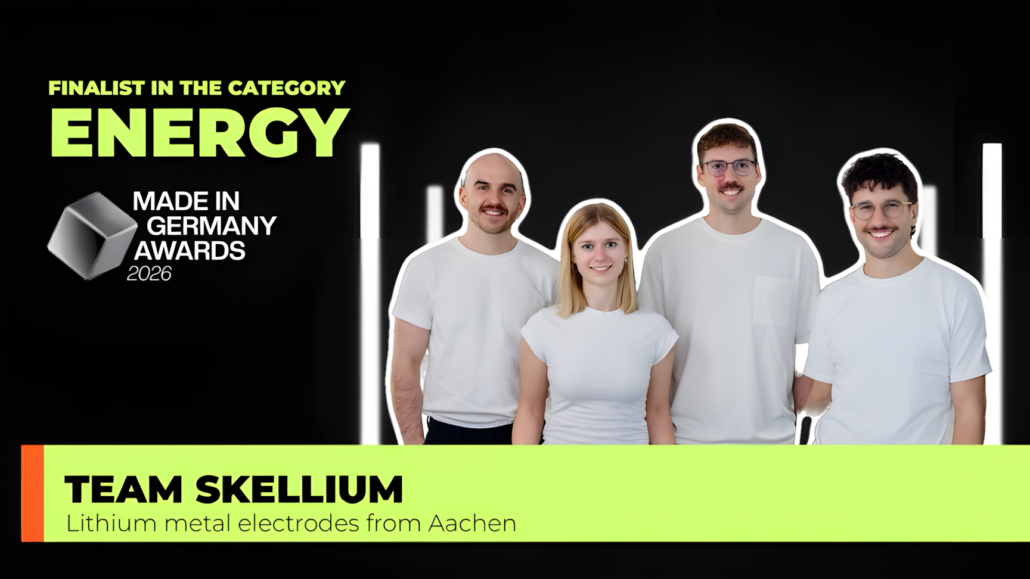
Aachen-based Skellium applies liquid lithium directly onto the copper current collector. Co-founder and CEO Gerrit Bockey on the idea behind the process, the biggest technical hurdle and the initial target market. Around 3,860 mAh/g and the lowest standard potential of any anode material: on paper, lithium metal has ideal properties for an anode. On the factory floor, things look different. Thin lithium foils are expensive, delicate and difficult to process. Skellium, a spin-off of the PEM institute at RWTH Aachen University, therefore relies on liquid lithium and has reached the finals of the Made in Germany Awards in the Energy category. Excerpt from the Breaking Lab video on the Made in Germany Awards (German audio, English subtitles). The full video with all three finalists is available on YouTube. The interview Gerrit, how did you come up with the idea for Skellium? My background is in production engineering. At PEM, we spent a lot of time on how to bring new cell concepts into mass production, and with lithium metal I kept getting stuck at the same point. The material is there, but the thin foils you need are expensive, hard to process and in limited supply at scale. At some point the question came up: why do we first roll lithium into a foil and then laminate it onto copper, instead of applying it directly where it belongs? That is where the melt process came from, and ultimately Skellium. What do you do differently from other approaches to lithium metal anodes? There are essentially two established routes. You can extrude and roll lithium, or you can deposit it from the vapor phase in a vacuum. With rolling, things get harder and more expensive the thinner the foil gets. Vapour deposition delivers very thin layers, but it needs a vacuum and is comparatively slow. We apply liquid lithium onto the copper foil under inert gas and without a vacuum. This allows us to produce layers between 3 and 50 micrometers thick directly on the current collector. Our goal is to further scale up the process in web width and speed. What benefits have you demonstrated so far? In our comparisons, lithium plating and stripping are more uniform than with the reference materials tested. We also create 3D structures in situ during production. These structures can inhibit dendrite growth. Tests with ester-based electrolytes achieved up to 200 percent more cycles. What was the biggest technical hurdle? Temperature control. The layer should solidify exactly when it has reached the target thickness, and do so reproducibly across the entire web. We invested a lot of time in keeping the temperature zones in the equipment separate and controlling them precisely. Then there is the atmosphere: liquid lithium reacts not only with oxygen and moisture but also with nitrogen, so everything runs under inert gas. These may sound like minor details, but they determine the quality of the coating. Who needs your anode first? In the short term, we see the biggest demand in prelithiation. Silicon and graphite anodes lose lithium in the first cycle, and a defined lithium layer can compensate for that loss. That market already exists today. In the medium term, it is about true lithium metal anodes for solid-state and lithium-sulfur cells. They need exactly the thin, uniform layers we are working on. Where do you stand today, and what is the next milestone? We currently produce coated samples for testing on our own line in Aachen. The line produces lithium and lithium alloy anodes at speeds of up to 5 m/min under inert gas, with an adjustable surface layer. Our next milestone is a new generation of equipment, which will let us coat both sides and produce larger quantities. We build in a modular way and extend the line with every milestone instead of starting from scratch each time. That lets us respond quickly to what we learn from the cells. And what do the Made in Germany Awards mean to you? For a topic like ours, they offer a valuable opportunity. Breaking Lab explains technology in a way that people outside the industry understand too, and that rarely happens with battery production. How to vote About Skellium Skellium is a spin-off of the PEM institute at RWTH Aachen University. The company develops lithium metal electrodes and the corresponding production technology for next-generation battery cells.

Skellium Develops Lithium Metal Anodes Using Melt Coating Read More »

Second Life for Power Tool Batteries: Potential Remains, but Recycling is still the main path

About half of the spent lithium-ion batteries collected from power tools are not deeply discharged. Yet only a small share can currently be refurbished economically. The EASLi research project examined which recovery route makes sense for different batteries—and found that earlier, more effective sorting is key. Led by Stiftung GRS, a consortium of companies across the battery value chain and end-of-life management sector examined the technically and practically viable options for spent nickel manganese cobalt (NMC) lithium-ion batteries from power tools. Project partners included Robert Bosch Power Tools, Gemeinsame Rücknahmesystem Servicegesellschaft mbH, Battery Damage Service (BDS), Erlos Produktion und Montagen GmbH, and ECOLOGICON GmbH. The German Federal Environmental Foundation (DBU) funded the project from January 2025 through February 2026. The work focused on three pathways: refurbishing batteries for a second service life (Loop 1); high-value hydrometallurgical recycling that can return recovered materials to cathode production (Loop 2); and pyrometallurgical processing to recover lower-grade secondary raw materials (Loop 3). What comes back through collection systems Three sorting campaigns examined more than four metric tons of material collected at take-back sites, including recycling centers and home improvement stores. Lithium-ion batteries accounted for approximately 55% of the power tool batteries examined. Nickel-cadmium (NiCd) batteries still made up 37% of that fraction, reflecting the continued return of older products—even though NiCd batteries have been prohibited in power tools placed on the market since 2017. The high NiCd share illustrates how long power tool batteries can remain in circulation. For the roughly one-quarter of batteries with an identifiable manufacturing year, the average time between manufacture and collection was about ten years. The oldest dated back to 1989. Batteries used by private consumers were returned after approximately eight years, compared with about four years for those used commercially. Technical potential remains Overall, around 70% of the sorted power tool batteries were deeply discharged, a figure driven largely by older NiCd batteries. By contrast, about half of the lithium-ion batteries were not deeply discharged, and newer batteries tended to retain a higher state of charge. In other words, today’s recycling stream includes batteries that may not have reached the end of their useful technical life and could warrant further evaluation for reuse or second-life applications. To assess how many batteries might actually qualify for reuse, BDS tested 265 used 18-volt battery packs. The evaluation process ranged from visual inspection and pack- and cell-voltage measurements to state-of-health (SoH) testing through charge-discharge cycling. The findings were sobering: 62% of the packs were deeply discharged, and more than one-third registered below 4 volts—an indication of potentially irreversible cell damage. The subsequent SoH assessment examined two distinct return streams: one closely linked to a manufacturer and another collected through a take-back system. In the respective subsamples, 30% and 11% of the battery packs were deemed suitable for reuse. Because those subsamples comprised only 64 and 19 packs, respectively, the findings cannot be considered representative of either return stream as a whole. Why reuse has yet to become a viable business model Low reuse rates pose a major challenge to economic viability. Under the study’s scenario, which assumed German labor costs, the expense of testing and measurement equipment would likely exceed the revenue generated by reselling reusable battery packs. According to the final report, making the process commercially scalable would require more targeted presorting, automation of individual testing steps, or different terms for acquiring used batteries. Regulatory obstacles add to the challenge. When end users discard batteries for disposal, those batteries are classified as waste and may be transferred only to certified waste-management companies. Power tool manufacturers generally do not hold the relevant certifications. Questions also remain about liability, warranties, and the branding under which refurbished batteries could be sold. In addition, uniform standards for testing and reuse are lacking. Battery design presents another obstacle. Power tool battery packs are engineered for durability and safe operation, not easy disassembly. Adhesives and a wide range of materials make refurbishment more difficult. The project’s final assessment is therefore cautious: second-life applications are technically feasible, but significant regulatory, practical, and economic barriers continue to prevent widespread adoption. High-value recycling is likely to handle the largest share The project team expects most end-of-life NMC power tool batteries to enter Loop 2, provided that sufficient identification and sorting capabilities are available. Refurbishment is expected to account for the second-largest share, with pyrometallurgical processing handling the smallest. Trials conducted by ERLOS yielded practical findings for Loop 2. Because battery management systems generally prevent complete discharge, the company tested a wet-discharge process that reduced battery-pack voltage to below 1 volt within 24 hours. Adding a zinc salt reduced corrosion. The trials also indicated that mixed batches of NMC and nickel cobalt aluminum (NCA) batteries can be directed into the same hydrometallurgical recycling stream under Loop 2. For process quality, contamination from materials such as plastics and electrolyte residues matters more than the precise cathode chemistry. This makes early separation of lithium-ion batteries from other battery types particularly important. Three decision points instead of one matrix EASLi originally set out to develop a multicriteria assessment system to identify the optimal recovery route for each battery. Over the course of the project, however, it became clear that such a matrix would be of limited practical use: collection sites, sorting facilities, and refurbishment companies have access to different information and face different operational decisions. The team instead developed decision trees for three points along the process where those decisions are actually made. At a collection site, basic questions can guide an initial assessment: Can the battery chemistry be identified? Is the housing damaged or contaminated? Are the contacts intact, and is the manufacturer identifiable? Sorting facilities distinguish between battery chemistries, while refurbishers additionally assess state of charge and SoH. The approach is intended to help smaller companies direct batteries toward appropriate recovery pathways without extensive data collection. EASLi thus addresses an often-overlooked aspect of battery recycling: the quality of recovered materials depends not only on the recycling technology itself, but also

Second Life for Power Tool Batteries: Potential Remains, but Recycling is still the main path Read More »

Beyond the Headlines: Battery News Expands Its Coverage With a New Video Format

Battery technology is complex—and simple answers often fall short. Battery News is expanding its coverage with a new video format: On YouTube, battery researcher Merlin Frank explains what is behind the latest developments, drawing on data and scientific evidence while keeping the content accessible. Whether the topic is service life, recycling, raw materials, or new cell technologies, batteries generate plenty of headlines—but not always enough context. That is where the new format comes in. Merlin Frank, a doctoral researcher at RWTH Aachen University, aims to explain what the numbers, studies, and technological developments actually mean. Less hype, more data. Batteries are no longer just a component of electric vehicles. They play a central role in mobility, energy supply, and industry—and are the subject of intense debate. Range, aging, raw materials, recycling, safety, and the global technology race involving Europe, China, and other regions regularly make headlines. With the new video offering, Battery News will also cover these topics in a format that provides more room for data, background, and technical context. Merlin Frank will be the face of the series. The doctoral researcher at RWTH Aachen University wants to show what lies behind the numbers, studies, and technological developments. Between Oversimplification and Technical Jargon One challenge, in Merlin Frank’s view, is how battery topics are often communicated. At one end of the spectrum are highly simplified explanations; at the other are highly specialized technical articles that can be difficult to follow without substantial prior knowledge. The new format is designed to bridge that gap. “My aim is to combine the two: technically rigorous and data-driven, but explained in a way that viewers without extensive prior knowledge can follow,” says Merlin Frank. Wherever possible, claims will not rest on isolated examples or personal assessments. Studies, market data, and Frank’s own analyses will provide the basis for putting figures and developments into a broader context. That is particularly important when it comes to batteries, because many questions cannot be answered simply as “good” or “bad.” How sustainable a battery is depends, for example, on its cell chemistry, manufacturing, use, electricity mix, service life, and end-of-life recycling. Claims about technological competitiveness or raw-material dependencies also require context. Rather than offering simple answers, Merlin Frank wants to make clear what conclusions the available data support—and where the evidence does not allow for a definitive judgment. From Cell Chemistry to the Battery Market The video format will cover a broad range of topics. Planned content includes foundational videos on subjects such as cell chemistries, battery design, aging mechanisms, and charging behavior. Data-driven market analyses and manufacturer comparisons will also play an important role. Merlin Frank also plans to address current developments, including new battery technologies, recycling processes, manufacturing sites, and developments among European and Asian battery manufacturers. The format therefore spans both foundational knowledge and current industry analysis. On-location reporting is also planned for the future. Merlin Frank aims to visit research institutions, companies, and industry events to show technological developments where they are being created and put into practice. Not Just for Battery Experts The target audience is intentionally broad. The videos are aimed at technically curious viewers and EV drivers as well as students, engineers, and professionals working with batteries, electric mobility, or energy technology. The key requirement is not a particular level of technical expertise, but an interest in understanding technological developments in greater depth. Merlin Frank wants to preserve technical depth without assuming that viewers are already experts in electrochemistry or battery production. Complex concepts should become easier to understand without being simplified to the point that important distinctions or uncertainties are lost. One Topic per Week As a rule, one new video is planned per week. Most episodes will run about 10 to 20 minutes, while more extensive analyses may be longer. The videos are intended to stay concise enough to address individual questions in a focused way while still leaving enough room for context and data. The new offering expands Battery News coverage with a format for anyone who wants to go beyond the headline when it comes to batteries: less hype, more data—and more room to understand what is really happening technologically. To the YouTube channel

Beyond the Headlines: Battery News Expands Its Coverage With a New Video Format Read More »

Controlling cathode drying efficiently: How precise dew point measurement reduces energy costs

In battery production, process stability is becoming an increasingly important factor in competitiveness. Cell manufacturers are under pressure to ramp up production capacity quickly, reduce energy consumption, and ensure consistently high product quality. This makes it especially worthwhile for German and European gigafactories to take a closer look at one particularly energy-intensive process step: cathode drying. Cathode drying can account for up to 45% of energy consumption in the dry room, making it a significant opportunity for optimization. By measuring moisture precisely and controlling the process reliably, manufacturers can use energy more efficiently, avoid overdrying, and secure product quality. In this free 30-minute on-demand webinar in German, Vaisala expert David Dlugay explains how battery manufacturers can better monitor and optimize cathode drying. The webinar addresses typical challenges in cell production: very high temperatures, aggressive chemicals, ultra-dry environments, and the risk of costly production interruptions. You will learn: The webinar is designed for engineers, process owners, and operations managers in battery manufacturing, dry room operation, and industrial energy management. Register now for free and watch on demand:Effiziente Kathodentrocknung in der Batterieherstellung | Vaisala

Controlling cathode drying efficiently: How precise dew point measurement reduces energy costs Read More »

Merlin Frank on the Geladen Podcast: Who Benefits from the EV Boom?

Merlin Frank joins the latest episode of the German-language Geladen podcast. A battery researcher pursuing his PhD at PEM at RWTH Aachen University, Frank discusses who benefits from the growth of electric mobility. The conversation focuses on the relationship between automakers and their battery suppliers, as well as the role of Chinese battery cell manufacturer CATL. The selection of electric vehicles is growing. Yet different car brands often rely on the same battery suppliers. What does this mean for Europe’s auto industry? Where do dependencies arise, and which parts of the value chain remain with automakers? Frank explores these questions using a market analysis by PEM. It links European new vehicle registration data with information on vehicles, battery systems, and cell suppliers. The conversation also examines which battery improvements matter in everyday use: longer range, lower costs, or other technical features. Listen to the full Geladen podcast episode featuring Merlin Frank (in German). More from Merlin Frank: “Im Spannungsfeld” Frank offers further scientific insights on his new YouTube channel, “Im Spannungsfeld,” powered by Battery-News. He explains the science behind batteries, electric mobility, and the circular economy. His goal is to make these technologies understandable while examining both their potential and their limitations. The channel’s content is in German. Visit the “Im Spannungsfeld” YouTube channel.

Merlin Frank on the Geladen Podcast: Who Benefits from the EV Boom? Read More »

Battery Cells “Made in Grünheide”: How Tesla Plans to Scale Cell Manufacturing in Europe

Starting in 2027, Tesla plans to produce its own 4680 battery cells in Grünheide and ramp annual capacity to as much as 18 GWh. While several battery cell projects across Europe have been delayed, scaled back, or halted, Tesla continues to invest in local manufacturing. Robert Meyer, Cell Factory Lead at Tesla Manufacturing Brandenburg, explains why the strategy is not just about cost, but also about resilience, expertise, speed, and greater control over the company’s own value chain. Why Europe, and Why Now? For Tesla, cell manufacturing in Grünheide is part of a broader principle: supply chains should be localized wherever possible, while manufacturing processes should be closely integrated both horizontally and vertically. According to the company, this is the model Tesla follows at its sites worldwide. At Gigafactory Berlin-Brandenburg, the focus from the outset was therefore not only on a high degree of vertical integration, but also on localizing as much of the supply chain as possible within Europe. “Localizing cell manufacturing puts us in a position to produce everything from the battery cell to the finished vehicle at a single site. That is unique in Europe,” Meyer says. From a purely economic perspective, however, the decision is far from an obvious one. Tesla acknowledges that battery cell manufacturing in Europe is currently difficult to justify in a direct cost comparison. Even so, the company remains committed to the plan. “From a purely cost perspective, the move offers limited advantages. For us, however, this is a strategic decision,” Meyer says. Tesla wants to strengthen supply-chain resilience, reduce dependencies, and at the same time expand vertical integration and manufacturing expertise at the site. From Learning in Texas to Ramp-Up in Grünheide Building a battery cell factory is not simply a matter of capital investment or installed capacity. The real challenge is whether complex processes can be translated reliably into high-volume production — with sufficient quality, high yield, and the shortest possible ramp-up time. Tesla sees an advantage here in not having to start from scratch. Lessons learned from 4680 production at its sister factory in Texas are expected to support the ramp-up in Grünheide. “The combination of high product and process complexity with high production volumes is a challenge,” Meyer explains. “But for the ramp-up of our cell factory in Grünheide, we benefit enormously from the fact that we have already solved this challenge at our sister factory in Texas.” Dry Electrode as a Key Technology The dry-electrode process plays a particularly important role. With dry coating, electrodes are manufactured without the conventional solvent-based wet process. For Tesla, the technology is a central element of its planned 4680 production in Grünheide. Because energy-intensive drying ovens are no longer required, Tesla says the process reduces both factory footprint and capital expenditure. It also eliminates costs associated with recovering toxic solvents. “The process not only has a noticeable positive impact on production costs, but also on the environmental footprint of manufacturing,” Meyer says. Another benefit is the significantly lower energy demand. Especially for battery cell production in Europe, more efficient processes could therefore become a decisive competitive factor. Vertical Integration Meets Europe’s Location Challenge Local cell manufacturing is also intended to make Tesla less dependent on a European supplier environment that, in the company’s view, is not yet comparable with the established battery ecosystems in Asia. Meyer points to Tesla’s factory in Shanghai, where the company sources cells from Chinese manufacturers and integrates them into its own vehicle production. “There simply isn’t a comparable ecosystem of manufacturers here that could serve as suppliers,” he says of Europe. At the same time, Tesla believes Europe is at a disadvantage in the global competition with China and the United States, citing in particular the absence of output-based incentives for battery cells in the EU. “In international competition, it is currently extremely difficult to manufacture cells economically in Europe,” Meyer says. From the company’s perspective, Europe needs clear and targeted framework conditions if battery cell technology is to become firmly established in the region over the long term. How Tesla Is Building Cell Manufacturing Expertise in Grünheide Alongside technology and capital, the ramp-up in Grünheide will above all be a workforce challenge. Tesla plans to hire more than 1,500 additional employees for cell manufacturing. At the same time, experienced battery cell manufacturing expertise remains scarce in Europe. Tesla is responding with a broad recruiting strategy. Prior experience in cell manufacturing is explicitly not a hiring requirement. “We are well aware that we are doing pioneering work here in Europe,” Meyer says. Tesla’s approach is to bring together people from different industries and with diverse professional backgrounds. Career changers can even be an advantage, he argues, because they may approach complex problems with a fresh and unbiased perspective. The strategy is supported by internal training and education programs. The Ramp-Up Playbook: Speed, Collaboration, and People What ultimately determines whether a gigafactory ramps successfully? For Meyer, speed comes first. “Speed is critical. We have to learn from our mistakes quickly and constantly ask ourselves whether a problem can be solved even faster.” That requires more than technical solutions. The organization itself also matters: teams need to collaborate closely across sites while retaining enough autonomy to make fast decisions. Striking the right balance between sharing best practices and maintaining local decision-making authority can accelerate the ramp-up process. Ultimately, however, Meyer traces the technical and operational challenge back to a classic factor: people. “To make such an ambitious project successful, you need highly motivated and committed employees who are all working toward the same goal.” Tesla at the Future Battery Forum 2026 Robert Meyer will continue the discussion on how battery cell production can be scaled successfully in Europe on November 24 and 25 at the Future Battery Forum at ECC Berlin. On the panel “The gigafactory scale-up playbook: Execution, yield, and speed,” he will join other international representatives from the battery cell industry. Tesla will also have its own booth at the Future Battery Forum and will
Battery Cells “Made in Grünheide”: How Tesla Plans to Scale Cell Manufacturing in Europe Read More »

Battery Testing Facilities in Europe

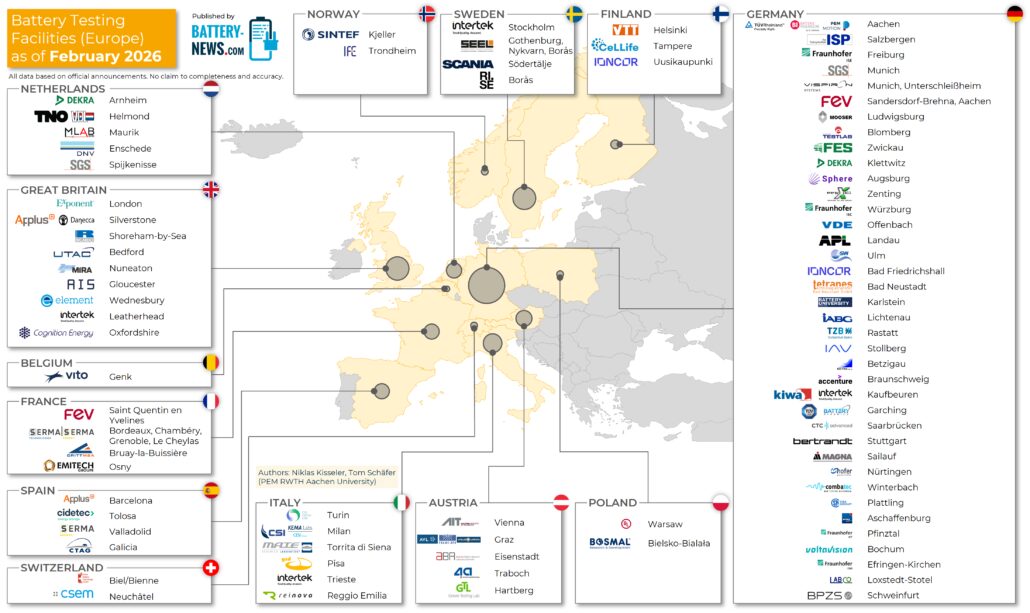
Battery-News presents an updated map of European testing facilities for batteries and battery systems in cooperation with the Chair of Production Engineering of E-Mobility Components (PEM) at RWTH Aachen University. The overview reflects the status as of February 2026 and was compiled by Niklas Kisseler and Tom Schäfer (PEM, RWTH Aachen University). Testing facilities across 13 European countries The map covers facilities in Germany, the United Kingdom, France, the Netherlands, Belgium, Spain, Switzerland, Italy, Austria, Poland, Norway, Sweden, and Finland. Germany has by far the largest concentration of entries, with additional locations across countries including the United Kingdom, France, and Italy. The overview includes specialized testing providers, research institutes, and in-house testing facilities. It illustrates the geographic distribution of Europe’s battery testing infrastructure. The underlying data comes from official announcements by the organizations listed and reliable battery industry sources. The map is available for free download in high resolution. This overview does not claim to be exhaustive. The editorial team welcomes corrections and additions through the contact form.

Battery Testing Facilities in Europe Read More »

E-Mobility Production Awards: Applications for the Community Award Open Until October 1st

The E-Mobility Production Awards will be presented for the fourth time on October 20, 2026, at the Battery Production Days (BPD) in Aachen. Prizes will be awarded in three categories: the Jury Awards “Battery Production” and “E-Motor Production,” and the Community Award “Process Innovation in Battery Production – supported by VDMA Battery Production” The awards are presented by the PEM Institute at RWTH Aachen University, PEM Share and Berylls by AlixPartners. Applying for the community award Unlike the two jury awards, the community award is decided on the basis of submitted entries. Eligible are technologies and methods that improve the efficiency, quality, or sustainability of battery production. Applications can be submitted until October 1, 2026, using the Award-Website. An award committee will draw up a shortlist based on two criteria: degree of novelty, and benefit and potential. Applicants will find out on October 2, 2026, whether their innovation has reached the final round. Two-stage voting The finalists are decided in a two-stage vote. Online voting runs until October 18, 2026. The entries will then be presented as posters at the Battery Production Days on October 20 and put to a live vote on site. The awards will be handed over the same day from 6 p.m. at the BPD evening event in Aachen. Attending the Battery Production Days is a prerequisite for taking part in the live vote and the award ceremony. Tickets and further information are available at battery-production-days.de.

E-Mobility Production Awards: Applications for the Community Award Open Until October 1st Read More »

Scroll to Top